Shaped Grinding & Finishing Media
Shaped grinding and finishing media are non-spherical process bodies selected to change contact, access or movement in a defined process. Cylinders, satellites, bicones and other forms are not interchangeable solely by nominal size. Identify particle-processing or workpiece-finishing duty, equipment, media material and geometry, target result, lodging and separation constraints, and acceptable wear chemistry before selecting or quoting a shaped-media charge.
- Material / construction
- Specified metallic or ceramic media; shape, formulation and size distribution reviewed
- Specification basis
- Drawing, diameter & acceptance
- Order basis
- Sample & production quantities
Shaped Grinding & Finishing Media: selection overview
Shape is a functional choice rather than a decorative variation on a ball. It changes how a medium contacts a surface, moves through a process and separates from the work. A form that reaches a recess can also lodge in a hole or damage an edge, so access and retrieval must be assessed together. Metallic burnishing shapes and abrasive ceramic finishing forms also have different mechanisms. Keep the media's formulation visible and define the process objective before comparing shapes. No single cylinder, satellite or bicone is asserted to improve every milling or finishing operation.
Choose shape from the work geometry or process need
For surface finishing, provide a drawing or sample showing holes, slots, recesses and surfaces that must remain protected. Define whether contact access or a specific edge result is the objective. For particle processing, describe the equipment and formulation separately instead of applying a deburring rationale to a milling charge. Name the proposed shape with actual dimensions or a drawing, because descriptive labels alone may conceal different profiles and contact features between suppliers.
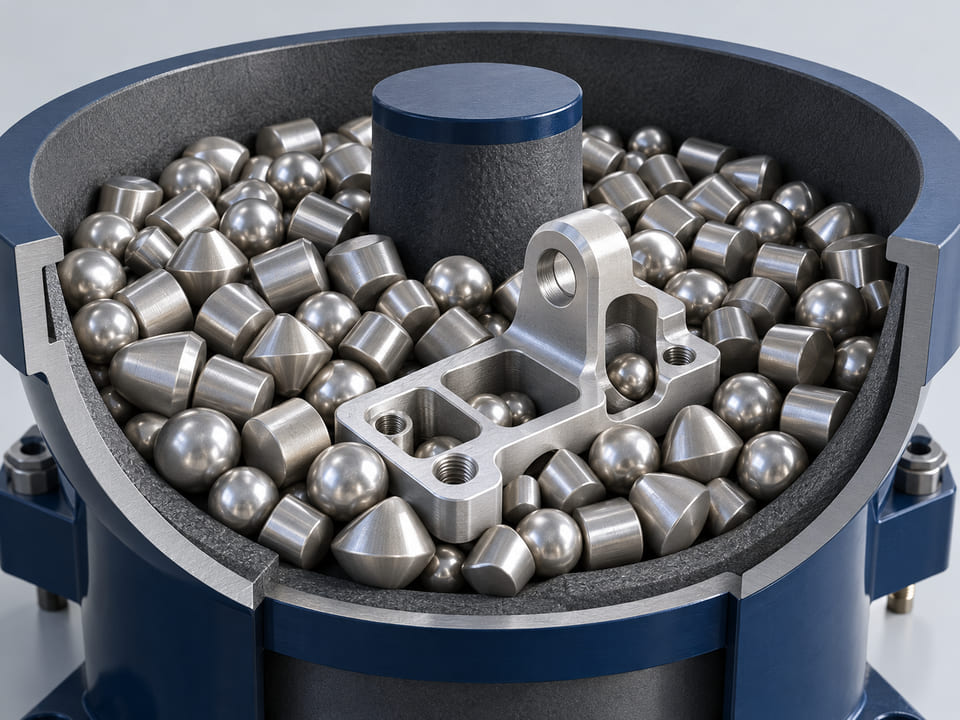
Validate lodging, wear and separation
A trial should evaluate more than the initial finish. Check whether media remains trapped, carries over into parts, changes shape as it wears or becomes difficult to separate. Define the acceptable size distribution and how undersize media will be controlled. Include contamination, breakage and the required cleaning result. A shape that cuts efficiently but cannot be reliably removed from the component may be unsuitable even if the first surface result looks attractive.
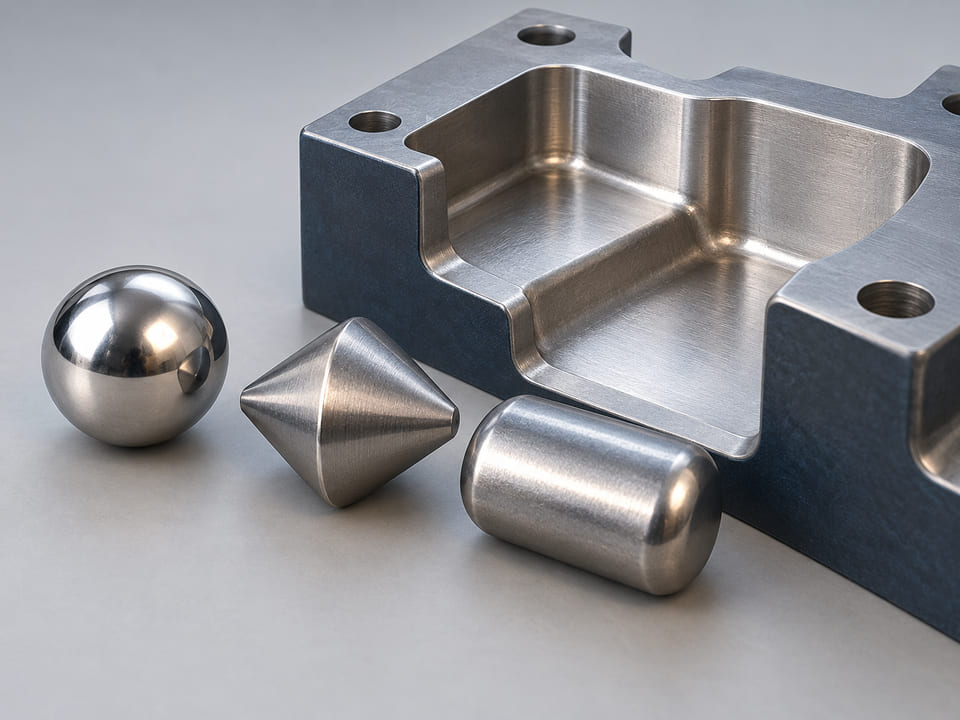
Shaped Grinding & Finishing Media specifications
Define the component using the requirements below. Include your target values and acceptance method; the quotation records the agreed material, geometry, inspection and supply scope.
| Requirement | What to specify | Why it matters |
|---|---|---|
| Process role | Identify particle processing, abrasive finishing or burnishing. | Shape selection must address a defined outcome and contact mechanism. |
| Shape drawing | Provide profile, dimensions and accepted distribution. | A name such as satellite or bicone does not uniquely identify geometry. |
| Workpiece or formulation | Include holes, recesses, protected surfaces or process chemistry. | Contact access and wear chemistry depend on the actual work. |
| Separation and trial | Define lodging, carryover, wear, breakage and target-result acceptance. | A useful finish is insufficient if the media cannot be reliably removed or controlled. |
Drawing and dimensional acceptance
Provide the drawing revision and nominal dimensions with units. Identify critical form, surface and fit requirements individually; a material designation alone does not define a finished component. Where an existing sample is the reference, describe wear and confirm the intended acceptance limits.
Order and inspection scope
Separate sample quantities from production demand. State the required inspection documents, lot identification, cleanliness and packaging. Any proposed substitute or change to the component specification should be reviewed before approval, with the quotation confirming the agreed scope.
Numeric performance values, when needed, must identify their material, conditions and evidence. Typical raw-material data should not be treated as guaranteed finished-component performance.
Shaped Grinding & Finishing Media applications
Start with the actual mechanism and exposure conditions. Each use below identifies the information needed for a useful technical review.
Contoured-part finishing
Shaped media may be considered where spheres do not provide the needed contact with a recess, edge or external contour. Review access and lodging together. Test representative parts with the proposed formulation and geometry, then inspect protected features, edge change and residual media rather than judging only the most visible external surface.
Burnishing and pressure-contact concepts
Specified metallic shapes may be reviewed for a defined surface-contact process. Distinguish non-abrasive smoothing from abrasive stock removal, and include the allowable dimensional change. Shape, part material and equipment interact, so the result should be established by a representative trial rather than an unrestricted statement that shaped media polish better.
Specialised particle-processing trials
A non-spherical medium can enter a process comparison where the equipment and formulation justify that geometry. Define the particle target and allowable wear chemistry separately from a finishing application. Compare the process outcome and charge behaviour under representative conditions instead of selecting a shape from a generic contact-area claim.
Compare Shaped Grinding & Finishing Media alternatives
Compare the requirement that drives the decision. A matching nominal diameter or similar appearance does not establish material or functional equivalence.
| Alternative | When to review it | Tradeoff to assess |
|---|---|---|
| Spherical media | Compare spheres when broad movement, simple contact and the intended process result can be achieved without a specialised profile. | Spherical and shaped media still need the same process acceptance; a simpler geometry may be preferable if it avoids lodging or separation problems. |
| Alumina media | Review a specified alumina media grade where abrasive formulation, wear chemistry and ceramic density suit the process objective. | A material label does not define shape or cut behaviour; evaluate the actual form, distribution and workpiece or formulation. |
| Zirconia media | Consider zirconia when its specific material profile and permissible contamination make it a relevant process-media alternative. | Distinguish spherical media from a shaped-media proposal and validate the actual charge, because composition alone does not predict access, lodging or separation. |
These links open the corresponding product pages in this collection. Final selection depends on your complete specification and the agreed validation.
Shaped Grinding & Finishing Media FAQs
Why choose shaped media instead of balls?
A specific shape may provide contact or movement useful to a defined process, particularly around workpiece features. The benefit must be demonstrated with the actual geometry and formulation. Shape is not a universal performance upgrade, and a useful contact profile can introduce lodging or separation problems that spheres avoid.
Are cylinders, satellites and bicones interchangeable?
No. Their profiles, contact and movement differ, and the names may not uniquely define dimensions between suppliers. Provide a drawing or approved sample and state the process objective. Compare the actual geometry and outcome instead of treating every non-spherical medium as one equivalent product.
How can media lodging be assessed?
Use representative parts and the proposed media distribution in a relevant trial. Check holes, slots, recesses and retention points, then evaluate separation and cleaning. Consider how worn or undersize media behaves as well as the new charge, because a profile that initially clears a feature may change with use.
Does shaped media always remove more material?
No. Formulation, equipment, contact and process objective all matter. Some shapes serve non-abrasive smoothing or specific access rather than aggressive removal. State the required edge or surface result and allowable dimensional change, then use a representative trial rather than a general contact-area or polishing claim.
Can the same media be used for milling and deburring?
Do not assume that. Particle processing and workpiece finishing have different objectives and acceptance methods. Identify the equipment, formulation or part and required result. Material chemistry, shape and wear should be reviewed for that role rather than transferring a successful deburring shape into an unrelated milling process.
What should a shaped-media quotation include?
Provide the process objective, equipment, media material and shape drawing, quantity and intended charge or batch context. Add the workpiece or formulation, target result, contamination limits and lodging or separation acceptance. Those inputs allow a specific media proposal and trial plan to be reviewed without inventing a universal process recipe.
Request a quotation
Turn the Shaped Grinding & Finishing Media requirements into a clear enquiry for MEITUO Balls.
- Define the material and geometry.
- Describe the application and acceptance.
- Separate sample and production demand.
The quotation confirms feasibility, supply scope, inspection documents and commercial terms. Generated illustrations are not evidence of available stock or completed validation.
Continue your material review
Engineering references and illustration notes
Material-family references support screening. The exact grade, finished geometry and application acceptance govern an actual enquiry.
CGI illustrations explain product, application or structure concepts. They are not photographs, measured micrographs, assembly drawings or inspection results.